As standardization evolves across the occupational safety, healthcare, and household cleaning sectors, the sealing integrity, convenience, and storage safety of disposable protective glove packaging have become pivotal to brand quality enhancement. The resealable flip-top bag for nitrile gloves—a new type of packaging designed specifically for disposable nitrile, medical-grade, and industrial safety gloves—has emerged as a mainstream choice in the protective equipment industry. Its popularity stems from advantages such as easy opening, resealability, protection against dust and moisture, and compatibility with automated packaging lines. Anhui Longqiang New Material Packaging Technology Co., Ltd. specializes in the R&D and production of innovative film and eco-friendly materials. Leveraging its technical expertise, the company provides high-quality, custom-made resealable flip-top bags for nitrile gloves, catering to diverse needs across medical, industrial, and household sectors with comprehensive, one-stop packaging solutions.
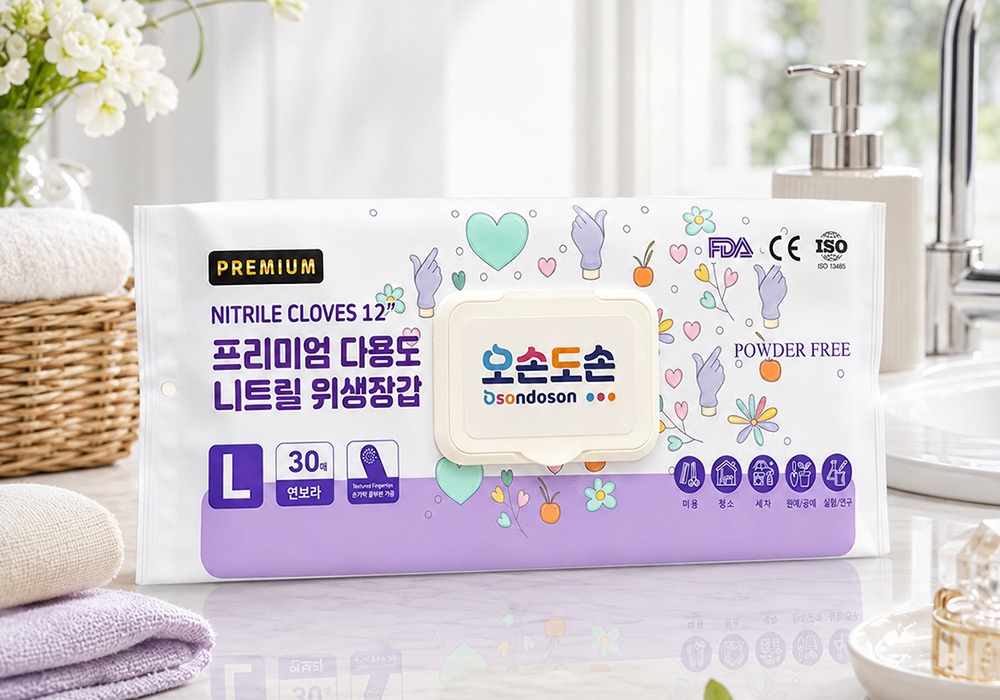
Conventional packaging for nitrile gloves typically utilizes a single-use heat-seal design that cannot be resealed after opening. This leaves remaining gloves exposed to air, making them susceptible to dust, moisture, and bacterial contamination—issues that lead to product waste and compromise both hygiene standards and the user experience. Longqiang’s resealable flip-top bags revolutionize traditional sealing methods with an innovative opening and closing mechanism. Users can easily open and reseal the bag as needed, effectively blocking external dust, moisture, and bacteria. This ensures the gloves remain clean and sterile over the long term, meeting the rigorous hygiene requirements for products such as medical masks, industrial safety gear, and sanitary supplies.
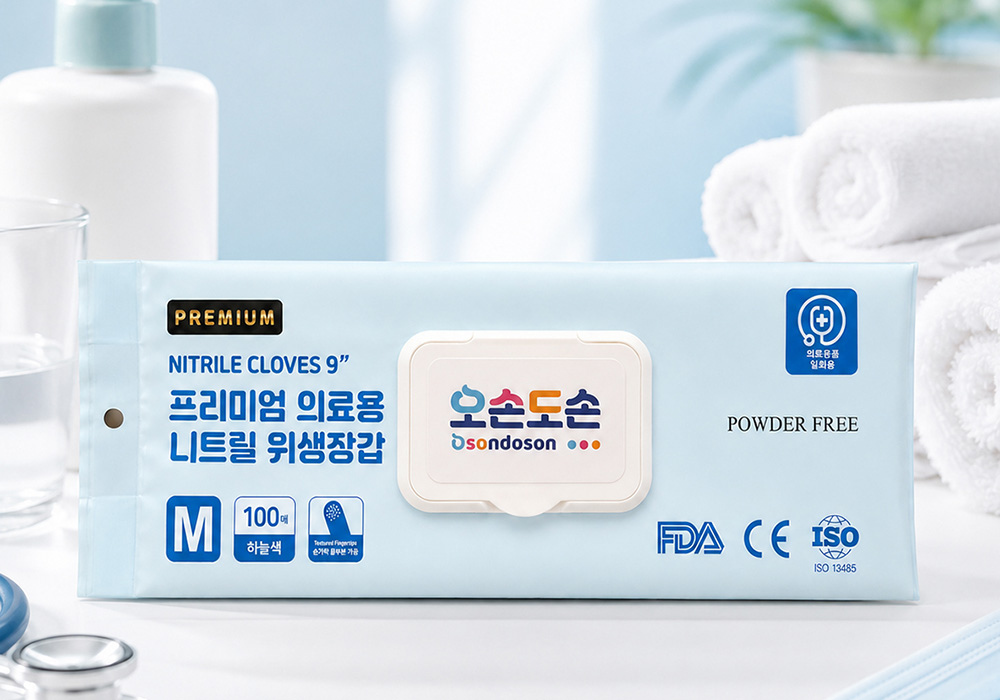
In terms of materials and manufacturing, these bags are crafted from the company’s proprietary, eco-friendly film materials. Produced using advanced, environmentally conscious processes, the bags are non-toxic, odorless, and safe. They offer exceptional toughness, tensile strength, and puncture resistance, ensuring durability against breakage or deformation. With superior sealing capabilities and outstanding resistance to moisture, dust, and oxidation, the bags effectively extend the shelf life of the nitrile gloves. Furthermore, the bags support high-definition printing and customization of logos, dimensions, and layouts. The resulting packaging is sleek and visually appealing with high color fidelity, simultaneously meeting functional storage and protection needs while elevating the brand’s overall image. These bags are ideal for the bulk packaging of nitrile gloves across various sectors, including industrial safety, healthcare, household use, and food processing.
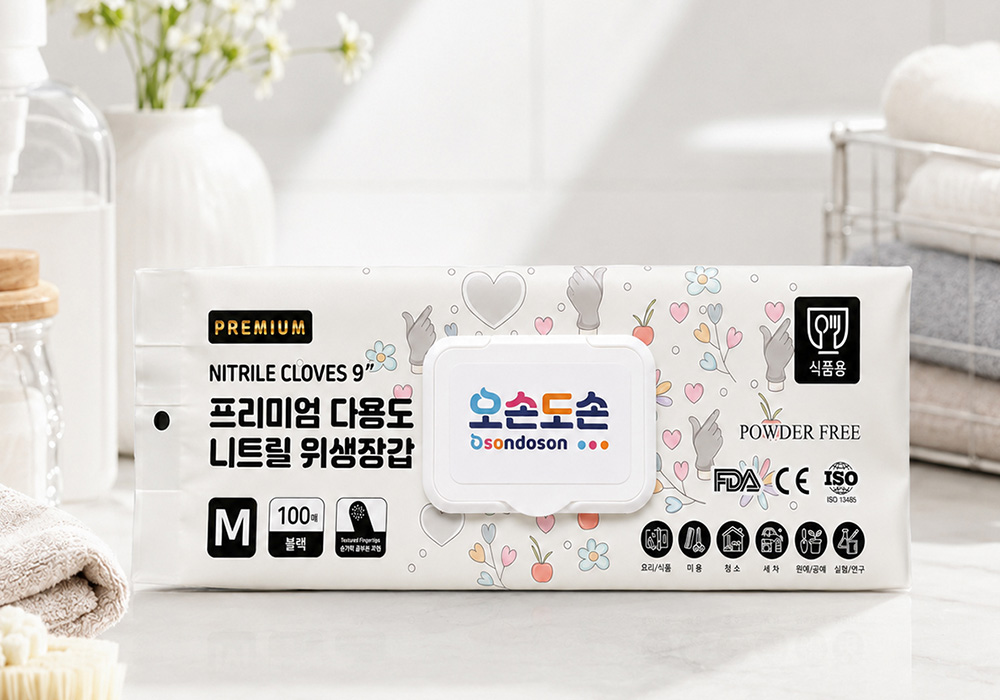
As a specialized enterprise in new-material packaging technology, Anhui Longqiang New Material Packaging Technology integrates R&D, process innovation, production and sales, and technical consulting services. Leveraging mature film production technology and comprehensive printing and packaging qualifications, the company strictly adheres to industry standards for decorative packaging printing and rigorously controls the quality details of every peel-and-seal pouch. Tailoring product structures and material properties to the specific packaging requirements of personal protective equipment, disposable medical supplies, and hygiene products, the company ensures regulatory compliance, safety, and practicality. By providing professional, end-to-end services—spanning material R&D and custom design to mass production—it empowers major protective equipment enterprises to upgrade their packaging and enhance product quality.