For products such as e-cigarette flavor capsules, fragrance beads, precision hardware components, and food flavorings, core packaging requirements include light shielding, aroma retention, moisture resistance, and oxidation prevention. Standard plastic bags fail to block light and air infiltration, easily leading to aroma loss, moisture-induced spoilage, and quality degradation. Aluminized bags for flavor capsules are specialized, high-barrier packages created using advanced composite film technology. Distinguished by their ability to shield light, retain aroma, resist moisture and oxidation, and provide superior sealing and a premium feel, they are the preferred choice for flavor capsules, fragrance consumables, and precision small parts. Anhui Longqiang New Material Packaging Technology Co., Ltd. specializes in the R&D and production of innovative film and composite coating materials, creating high-quality aluminized bags that elevate packaging standards through advanced material technology.
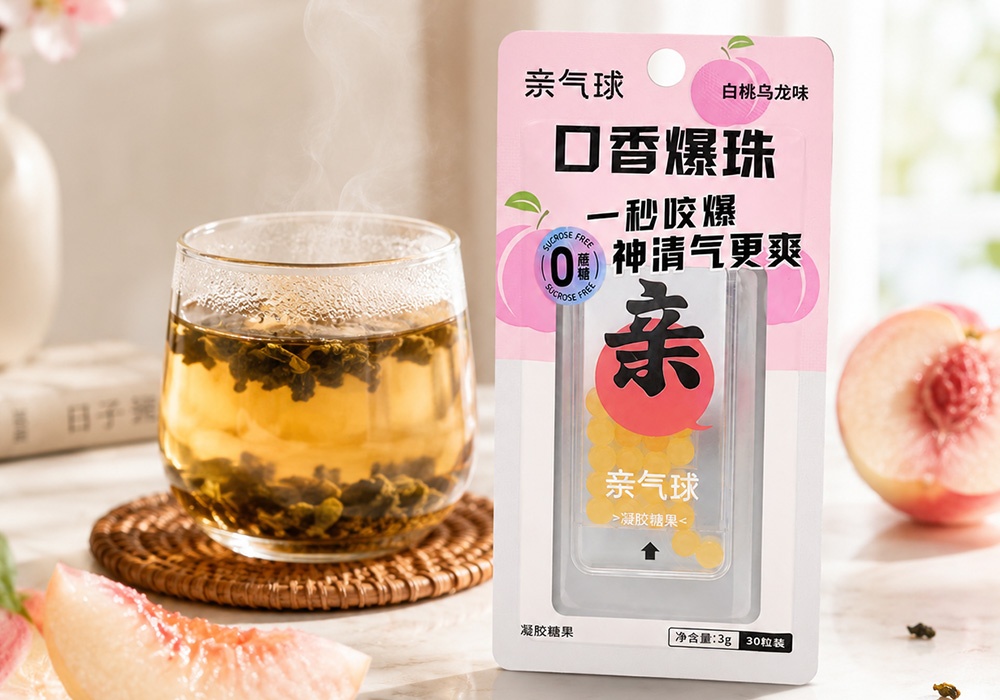
The primary challenges for flavor capsule products—such as aroma volatility, light-induced decomposition, and moisture-related spoilage—demand exceptional barrier performance from packaging. Longqiang’s aluminized bags utilize a multi-layer composite aluminization process combined with the company’s proprietary eco-friendly film materials. This creates a comprehensive, airtight protective system featuring a wear-resistant outer layer, an aluminized barrier middle layer, and a sealing inner layer that locks in freshness. The aluminized layer blocks 100% of UV rays and intense light, completely preventing the light-induced decomposition of capsule ingredients. Meanwhile, the multi-layer composite structure effectively blocks the infiltration of air and moisture, firmly locking in the original aroma and preventing loss, dampness, or oxidation, thereby significantly extending the product’s shelf life and storage stability.
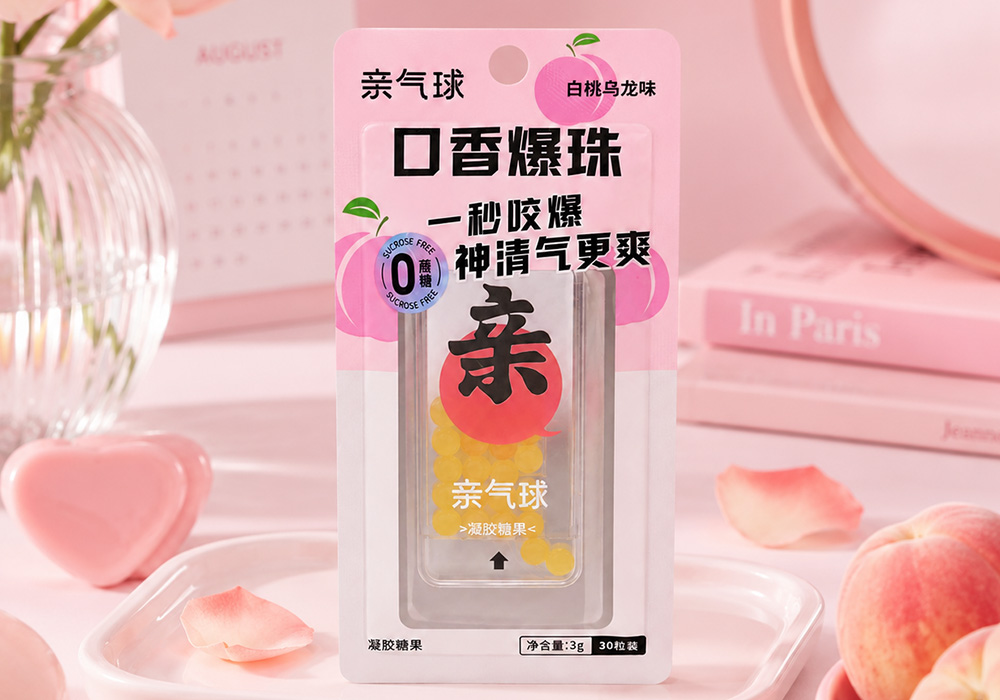
These bags offer outstanding advantages in both texture and practicality. With a smooth, refined surface and a premium metallic finish, they enhance the product’s high-end positioning and meet the needs of brands seeking to upgrade their packaging quality. The bags are exceptionally tough, tear-resistant, and durable against handling, minimizing risks such as breakage, air leaks, or bulging, making them ideal for mass production, long-distance transport, and long-term storage. We offer personalized processing options—including custom sizes, unique bag shapes, color printing, anti-counterfeiting features, and matte finishes—allowing for bespoke packaging tailored to specific product specifications and brand identities. Our solutions are suitable for a wide range of items, such as e-cigarette flavor capsules, aromatherapy beads, fragrance granules, and small precision consumables.
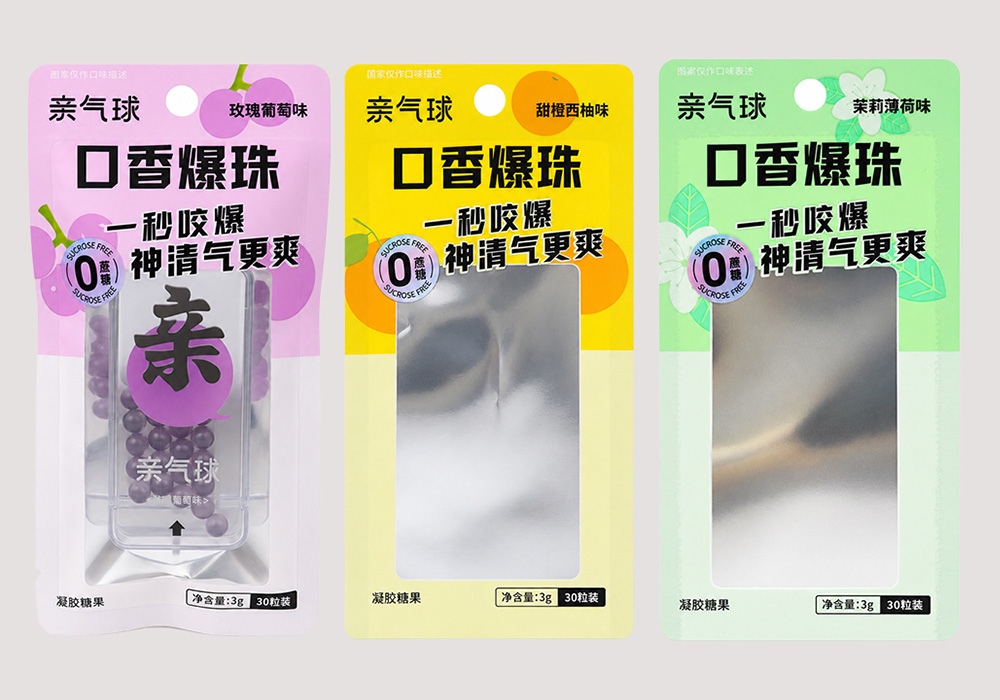
Deeply rooted in the new-material packaging sector, we continuously drive R&D, process innovation, and technological advancement. Leveraging mature production systems for rubber and plastic products alongside advanced film materials—and backed by compliant packaging and printing certifications—we manage the entire production lifecycle of aluminized capsule pouches in-house, from material development and lamination to aluminizing, custom printing, and final product output. This ensures consistent quality and exceptional cost-effectiveness. Furthermore, we continuously optimize material formulations and production processes to meet evolving market demands, providing clients with professional packaging consultancy and customized solutions that comprehensively address the protective and branding needs of high-end, precision products.